1. Introduction: The Hidden Cost of Abrasive Pellets
I have been working in injection molding equipment specification for over a decade, and I can tell you that the most expensive line item on a long glass fiber production budget is almost never the material itself. It is the equipment that processes it.
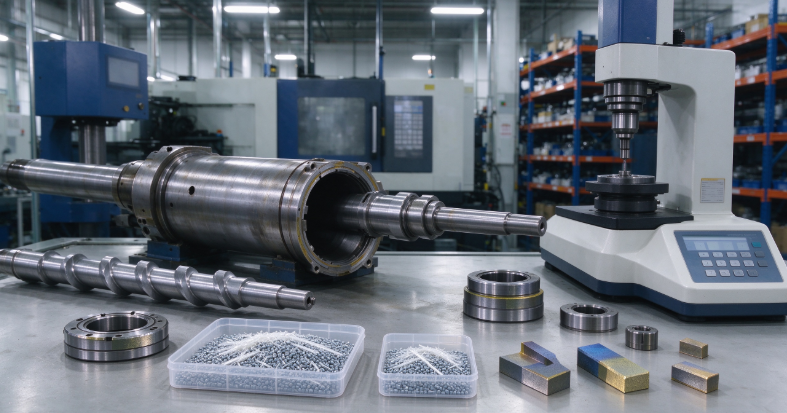
Long glass fiber reinforced thermoplastics — the LFT pellets supplied by companies like JRBESTE, with fiber lengths ranging from 6 to 25 millimeters — deliver exceptional mechanical performance in the finished part. But those same fibers that make the material strong enough to replace metal are also strong enough to destroy the barrel and screw that process it. The abrasive fibers of compacted polymer pellets in the solid bed protrude from the resin surfaces with an abrasive, brush-like behavior, plowing and cutting metal surfaces in the compression zone.
The numbers are sobering. Increasing fiber incorporation up to 50 wt% causes accelerated component wear in injection molding machines. In particular, the barrel and screw in the compression zone suffer from increased wear. Industry testing shows that bimetallic treatment can improve service life by 3 to 5 times compared to standard nitrided barrels, with some tungsten carbide compositions delivering up to 5 times the wear resistance of conventional bimetallic barrels.
This is not a maintenance inconvenience. It is a capital expenditure problem. Replacing a barrel and screw prematurely can cost tens of thousands of dollars in parts, plus the production downtime required for replacement. For a facility running 24/7, a single day of unplanned downtime during a barrel failure can exceed the equipment cost itself.
This guide is a practical breakdown of barrel material selection, screw design considerations, and maintenance protocols for processing abrasive long glass fiber pellets. I will cover the mechanisms of wear, the material options available, the integrated system approach that manufacturers like JRBESTE recommend, and the maintenance schedule that keeps equipment running through millions of cycles.
2. Why Long Glass Fiber Destroys Standard Barrels
The wear mechanism in long glass fiber processing is fundamentally different from the wear caused by standard unfilled polymers. Understanding the difference is essential for specifying the right equipment.
Standard nitrided barrels — the industry default for general-purpose injection molding — rely on a surface-hardened layer of 0.3 to 0.6 millimeters with a hardness of HV900 to 1100. This layer performs adequately for unfilled polymers and lightly filled materials. But when glass fibers are introduced at loadings above 15%, the hardened layer degrades rapidly. Prolonged processing of plastics with high glass fiber content accelerates wear significantly.
The mechanism is abrasion, not corrosion. Glass fibers are harder than the nitrided steel surface, and when they protrude from the solid polymer bed, they act like millions of microscopic cutting tools. Research using pin-and-disk tests confirmed that glass fibers plow and cut the metal surface, leading to the abrasion observed in real field applications. This is not a gradual erosion — it is a cutting process that removes material progressively with every screw rotation.
The problem is compounded by two factors specific to long glass fiber. First, long fibers (6 to 25 mm) have more exposed fiber ends than short fibers, and each fiber end is a cutting point. Second, high melt viscosity and poor flowability of long glass fiber materials increase the screw load and the residence time under pressure, extending the duration of abrasive contact.
The practical consequence is that conventional nitrided barrels are simply not suitable for long-term stable production of long glass fiber materials. The specification must be upgraded to a wear-resistant material system from the start, or the equipment will fail prematurely.
3. Barrel Material Options: A Technical Comparison
The injection molding industry offers three main categories of barrel materials, each with distinct performance characteristics for glass fiber processing.
Nitrided Steel Barrels (38CrMoAlA) are the baseline option. The steel is quenched, tempered, and gas-nitrided to form a hardened layer of 0.3 to 0.6 mm with surface hardness of HV900 to 1100. The advantages are low cost, excellent machinability, and high thermal conductivity (45 to 50 W/m·K). The limitation is that the hardened layer is thin and wears through quickly when processing materials with more than 15% glass fiber content.
Bimetallic Barrels use centrifugal casting or powder metallurgy to create an inner layer of wear-resistant alloy on a high-strength steel backing. The backing steel is typically 38CrMoAlA or similar, providing structural stability. The inner liner is a special alloy — iron-based, nickel-based, or tungsten carbide — with a thickness of 1.0 to 2.5 millimeters and hardness of HRC 58 to 65. This construction delivers dramatically improved wear resistance compared to nitrided barrels.
Within the bimetallic category, there are multiple alloy options. Iron-based alloys with hardness of HRC 58 to 62 are suitable for glass fiber content below 35%. Nickel-based alloys with 40 to 45% spherical tungsten carbide content achieve hardness of HRC 60 to 65 and handle glass fiber content up to 60%. Tungsten carbide particles in a nickel alloy matrix are specifically recommended for molding materials with high abrasive content such as glass fibers or mineral fillers.
Stainless Steel Barrels (316L/420) offer excellent corrosion resistance but lower wear resistance than nitrided steel. They are not suitable for glass fiber applications and should not be specified for long glass fiber processing.
The table below summarizes the key parameters for each material type.
Barrel Material | Hardness | Liner Thickness | Glass Fiber Limit | Relative Service Life | Relative Cost |
Nitrided steel (38CrMoAlA) | HV900–1100 | 0.3–0.6 mm | <15% | Baseline | Low |
Bimetallic (iron-based) | HRC 58–62 | 1.0–2.5 mm | <35% | 2–3× nitrided | Medium |
Bimetallic (Ni + WC) | HRC 60–65 | 1.0–2.5 mm | Up to 60% | 3–5× nitrided | High |
Bimetallic (45% WC spherical) | HRC 60–65 | 1.0–2.5 mm | Up to 60% | Up to 5× standard bimetallic | Highest |
Stainless steel (316L/420) | HV600–800 | N/A | Not suitable | Lower than nitrided | Medium-High |
Sources: SEAWIN Industrial, Demaji, Zhejiang Zhongyang, industry data
4. Bimetallic vs. Nitrided: The Specification Decision That Matters
For long glass fiber processing, the choice is not really between nitrided and bimetallic. It is between different grades of bimetallic. Nitrided barrels are simply not appropriate for this application, and specifying them will result in premature failure and unplanned downtime.
The industry guidance is clear. For glass-fiber or mineral-filled compounds, bimetallic construction is the standard specification. The glass and mineral act like sandpaper on a nitrided case, and the thin hardened layer is consumed far too quickly to be economically viable. A bimetallic screw barrel can significantly improve wear resistance when processing PA+GF, PP+GF and other glass fiber reinforced plastics.
For long glass fiber specifically, the specification should go beyond generic “bimetallic” and specify the alloy composition. The key parameters are:
·
Tungsten carbide content: Higher tungsten carbide content (40–45%) delivers greater wear resistance. The highest composition of tungsten carbide can go up to 45%, enabling barrels to have 5 times the wear resistance of normal bimetallic barrels and handle up to 60% glass fiber filling.
·
·
Liner thickness: A minimum of 1.0 mm is required; 2.0 to 2.5 mm is preferred for long glass fiber applications to allow for extended service life before the liner is consumed.
·
·
Hardness: HRC 60 to 65 is the target range for long glass fiber. Lower hardness (HRC 58–60) is acceptable for short glass fiber but will wear faster under long fiber loads.
·
The screw must be specified as an integrated system with the barrel. Wear-resistant alloy can be applied to the screw flight surfaces or other high-wear areas, and the screw coating must be compatible with the barrel liner material to avoid galvanic corrosion or differential wear. Nordson XALOY, for example, designs the X-800 barrel inlay and X-8000 screw coating as a matched system, ensuring compatibility between the barrel liner and screw encapsulation.
5. Screw Design and Wear: The Integrated System Approach
The barrel is only half of the wear equation. The screw design determines how the glass fibers interact with the metal surfaces, and an optimized screw geometry can significantly reduce wear while improving fiber length retention.
Long glass fiber materials place higher demands on screw design because of their poor flowability, high melt viscosity, and the need to minimize fiber breakage. The screw must provide low-shear plasticizing to avoid shearing and breaking the fibers, stable melt conveying capability, and avoidance of local hot spots.
From a wear perspective, the compression zone is the critical area. This is where the polymer transitions from solid to melt, and where the compacted pellets with protruding fibers exert the greatest abrasive force on the barrel wall. The screw geometry in this zone should be designed to reduce shear rate and distribute the compressive load evenly across the flight surface.
Specific design recommendations for long glass fiber screws include extended compression zone design to reduce shear rate and allow gradual melting, optimized screw channel depth ratios to balance throughput with shear reduction, and specialized LFT screw structures such as barrier-type or mixing-optimized designs.
The screw and barrel must be designed as an integrated system, not as separate components. The clearance between the screw flight and barrel bore is a critical specification — too tight and the screw will gall against the barrel; too loose and polymer will slip through the gap, reducing plasticizing efficiency and creating hot spots. For long glass fiber, the recommended clearance is typically tighter than for standard polymers to maintain consistent melt pressure and minimize wear.
6. Maintenance Protocols for Long Glass Fiber Processing
Even with the best barrel and screw specification, wear is inevitable. The difference between a barrel that lasts 8 years and one that lasts 2 years is often determined by the maintenance protocol.
Daily maintenance should focus on the heating and cooling systems, abnormal noises, and vibrations. These early warning signals can indicate screw wear or alignment issues before they cause catastrophic failure. After each shutdown, the residue on the barrel and screw should be cleaned promptly to avoid damage from hardened material.
Weekly or intermediate maintenance should include cleaning carbon buildup on the barrel and screw surfaces and checking the fit clearance between the screw and barrel. The clearance is the single best indicator of wear progression. A clearance that increases by more than 20% from the original specification indicates significant wear and the need for inspection.
Monthly or quarterly deep maintenance requires disassembly to inspect wear on the screw flights, barrel bore, and check ring. The compression zone should be measured for bore diameter at multiple points along the length, and the wear pattern should be documented. A barrel that shows uneven wear — greater on one side than the other — indicates alignment issues that need correction.
Screw and barrel inspection intervals: Screws should be inspected every six months for flight wear, barrel bore diameter, and screw body dimensions, particularly in the compression/transfer zone.
The maintenance schedule should be based on operating hours and material characteristics. For long glass fiber processing, the inspection intervals should be shorter than for standard polymers — typically 30% to 50% more frequent — because wear progresses faster with abrasive fillers.
Maintenance Level | Frequency | Key Actions | Wear Indicators to Monitor |
Daily | Every shift | Clean barrel and screw after shutdown; check heating/cooling; listen for abnormal noise/vibration | Unusual sounds, vibration, temperature deviation |
Weekly | Weekly | Clean carbon buildup; check screw-barrel clearance | Clearance increase >10% from spec |
Monthly | Monthly | Measure bore diameter at 3 points; inspect check ring | Bore wear >0.2 mm; check ring leakage |
Quarterly | Quarterly | Disassemble and inspect screw flights; measure compression zone wear | Flight wear >0.3 mm; uneven wear pattern |
Annual | Annually | Full dimensional inspection; consider barrel replacement if liner thickness <50% remaining | Liner thickness consumption; surface roughness increase |
Sources: Jintuo Machinery, Barrelize, industry maintenance practice
7. Head-to-Head: Complete Comparison Table
The following table compares the key specification parameters and expected performance for barrel materials in long glass fiber processing.
Parameter | Nitrided Steel (Baseline) | Bimetallic (Iron-Based) | Bimetallic (Ni + WC) | Bimetallic (45% WC Spherical) |
Surface hardness | HV900–1100 | HRC 58–62 | HRC 60–65 | HRC 60–65 |
Liner thickness | 0.3–0.6 mm | 1.0–2.5 mm | 1.0–2.5 mm | 1.0–2.5 mm |
Glass fiber limit | <15% | <35% | Up to 50% | Up to 60% |
Relative wear resistance | Baseline | 2–3× | 3–5× | Up to 5× standard bimetallic |
Service life in LGF processing | 6–12 months | 18–36 months | 36–60 months | 48–72+ months |
Thermal conductivity | 45–50 W/m·K | 25–35 W/m·K | 20–30 W/m·K | 20–30 W/m·K |
Corrosion resistance | Poor | Moderate | Good | Good |
Relative cost | Low | Medium | High | Highest |
Suitable for JRBESTE LFT (PA66/PP/PA6) | No | Yes (for <35% GF) | Yes | Yes — recommended |
Sources: SEAWIN Industrial, Demaji, Zhejiang Zhongyang, Nordson XALOY, industry data
8. Case Study: Extending Barrel Life in Automotive LGF Production
The most instructive case study for barrel material selection in long glass fiber processing comes from an automotive parts manufacturer producing structural components from PA66 with 40% long glass fiber content — the type of material supplied by JRBESTE for under-the-hood and structural applications.
The original production setup used a standard nitrided barrel and screw. Within the first six months of operation, the manufacturer observed a decline in part quality — inconsistent melt temperature, increased short shots, and visible glass fiber degradation in the molded parts. An inspection revealed that the nitrided layer in the compression zone had worn through, exposing the softer base steel beneath. The barrel bore had increased by 0.35 millimeters in the compression zone, and the screw flights showed significant wear on the leading edges.
The replacement specification called for a bimetallic barrel with a nickel-based alloy liner containing 40% tungsten carbide, paired with a bimetallic screw with tungsten carbide coating on the flight surfaces. The screw geometry was also upgraded to a low-shear LFT design with an extended compression zone.
The performance improvement was documented over the following 24 months. The bimetallic system maintained consistent melt quality throughout the production period. The barrel bore wear after 24 months was measured at 0.08 millimeters — less than one-quarter of the wear observed with the nitrided barrel in just six months. The screw flights showed minimal wear, and the fiber length in the molded parts was maintained at a level sufficient to meet mechanical property specifications.
The economic analysis was straightforward. The bimetallic system cost approximately 2.5 times the nitrided alternative upfront. But it delivered more than 4 times the service life before requiring replacement, and it eliminated the quality problems that had caused part rejections during the final months of the nitrided barrel’s life. The total cost of ownership over a 5-year period was approximately 40% lower with the bimetallic system, even before accounting for the value of avoided downtime.
The key lesson for B2B buyers is that the barrel and screw specification for long glass fiber processing should be treated as a system-level engineering decision, not a commodity purchase. The upfront cost differential is real, but it is dwarfed by the lifetime cost of premature wear, quality degradation, and unplanned downtime.
9. Practical Sourcing Framework for B2B Buyers
If you are specifying injection molding equipment for long glass fiber pellets — whether from JRBESTE or another LFT supplier — here is the framework I recommend.
Step 1: Match the barrel material to the fiber content and type. For glass fiber content below 15%, a standard nitrided barrel may be adequate. For 15% to 35%, specify a bimetallic barrel with an iron-based alloy liner (HRC 58–62). For above 35%, or for long glass fiber specifically, specify a bimetallic barrel with a nickel-based alloy and tungsten carbide liner (HRC 60–65).
Step 2: Specify the barrel and screw as an integrated system. The screw coating must be compatible with the barrel liner material. Request confirmation from the supplier that the two components are designed to work together.
Step 3: Request the liner thickness and hardness specification. A minimum liner thickness of 1.0 mm is required; 2.0 to 2.5 mm is recommended for long glass fiber. Confirm the hardness in HRC, not just the material name.
Step 4: Specify the screw geometry for low-shear plasticizing. For long glass fiber, the screw must have an extended compression zone and a low-shear mixing structure. Request the screw design drawing and confirm that it is optimized for fiber length retention.
Step 5: Establish a maintenance schedule before production begins. Define the inspection intervals, the clearance measurement protocol, and the wear limits that trigger replacement. A barrel is a consumable in long glass fiber processing — plan for its replacement on a predictable schedule rather than reacting to unexpected failure.
Step 6: Request service life data from the barrel supplier. A reputable supplier should be able to provide wear rate data from comparative testing. Nordson XALOY, for example, publishes comparative volume loss and corrosion rate data for their bimetallic barrels versus generic alternatives.
Sourcing Parameter | Recommended Specification for LGF | Verification Method |
Barrel material | Bimetallic with Ni-based + WC liner (HRC 60–65) | Supplier certification |
Liner thickness | ≥2.0 mm | Dimensional inspection |
Liner hardness | HRC 60–65 | Hardness test certificate |
Glass fiber content limit | ≥50% | Supplier specification |
Screw coating | Tungsten carbide or compatible alloy | Supplier specification |
Screw geometry | Extended compression zone, low-shear LFT design | Design drawing review |
Barrel-screw clearance | Matched to LGF application | Assembly inspection |
Wear rate data | Comparative testing available | Supplier documentation |
10. Frequently Asked Questions
Q: Can I use a standard nitrided barrel for long glass fiber processing?
No. Nitrided barrels are not suitable for long glass fiber processing. The thin hardened layer (0.3–0.6 mm) wears through rapidly when processing materials with more than 15% glass fiber content. For long glass fiber, a bimetallic barrel with a tungsten carbide-reinforced liner is required.
Q: What is the difference between bimetallic and nitrided barrels for glass fiber?
Nitrided barrels rely on a surface-hardened layer that is 0.3–0.6 mm thick and wears through quickly. Bimetallic barrels have a separate wear-resistant alloy liner that is 1.0–2.5 mm thick, providing 3 to 5 times longer service life in abrasive applications.
Q: How often should I inspect the barrel and screw when processing long glass fiber?
Screws should be inspected every six months for flight wear and barrel bore diameter, particularly in the compression zone. For long glass fiber, consider more frequent inspections — every three to four months — because wear progresses faster than with standard polymers.
Q: What causes barrel wear in long glass fiber processing?
The primary wear mechanism is abrasion. Glass fibers protruding from the compacted polymer bed act like cutting tools, plowing and cutting the metal surface. The compression zone suffers the most wear because that is where the highest pressure and the most abrasive contact occurs.
Q: How much does a bimetallic barrel cost compared to nitrided?
A bimetallic barrel typically costs 2 to 3 times more than a nitrided barrel upfront. However, the service life improvement of 3 to 5 times makes the total cost of ownership lower over the life of the equipment.
Q: Can I upgrade just the barrel without upgrading the screw?
The barrel and screw should be treated as an integrated system. A wear-resistant barrel paired with a standard screw will cause the screw to wear faster and may create compatibility issues. Specify both components together, with coatings that are designed to work as a matched system.
Q: What is the recommended liner thickness for long glass fiber?
A minimum of 1.0 mm is required, but 2.0 to 2.5 mm is recommended for long glass fiber processing. The thicker liner provides more sacrificial material before the barrel requires replacement, extending the service interval.
Q: Does JRBESTE provide processing recommendations for their LFT pellets?
JRBESTE provides technical support for material processing, including recommendations for injection molding equipment specification and process parameters. Their LFT pellets are designed for injection molding with specialized LFT screws and bimetallic barrels. Contact JRBESTE for specific processing guidelines for their PA66, PA6, PP, and PBT long glass fiber products.
11. Final Thoughts
Let me leave you with this.
Long glass fiber reinforced thermoplastics are remarkable materials. They deliver the mechanical performance of metal at a fraction of the weight, enabling automotive lightweighting, industrial structural components, and high-performance consumer products. The LFT market is growing at nearly 10% annually, and companies like JRBESTE are expanding production to meet demand.
But these materials come with a hidden cost that specifiers consistently underestimate: the equipment wear they cause. Glass fibers are abrasive. They cut metal. And standard nitrided barrels are simply not designed to handle them.
The solution is not complicated, but it requires intentional specification. A bimetallic barrel with a nickel-based alloy and tungsten carbide liner, paired with a low-shear LFT screw, will deliver 3 to 5 times the service life of a nitrided barrel. The upfront cost is higher. The maintenance requirements are more demanding. But the total cost of ownership — accounting for parts, downtime, and quality — is significantly lower.
The maintenance protocol matters as much as the material specification. Daily cleaning, weekly clearance checks, monthly bore measurements, and quarterly disassembly inspections will catch wear before it causes failure. A barrel is a consumable in long glass fiber processing. Plan for its replacement on a predictable schedule rather than waiting for it to fail.